A cabinet can look convincing in a product photo while its narrow edges tell a different story. Open the door, pull out a drawer, or look under a shelf: a lifted strip, a sharp corner, or a line of exposed board can quickly change how the whole piece feels. For buyers of nightstands, storage cabinets, and other panel furniture, edge banding is a small detail with an outsized effect on the delivered product.
The practical question is not simply whether the supplier uses an edge-banding machine. It is which edges receive which treatment, what the approved result looks and feels like, and how that result will be repeated across a production run.
Start with an edge map, not a material name
Edge banding is a separate strip applied to the narrow side of a panel. It finishes the exposed core and contributes to the cabinet’s appearance. Panel and edging suppliers offer different material and decorative options; EGGER describes ABS edging as a way to finish the narrow edges of decorative wood-based panels.
A specification that says only “matching edge banding” leaves too much open. The buyer should identify the substrate and surface first, then mark the treatment for each edge: the top and front of a bedside cabinet, door and drawer fronts, internal shelves, bottom edges, backs, and any exposed opening. A hidden edge may need a different visual finish from a high-touch front edge, but that distinction should be agreed before pricing and sampling, not discovered after assembly.
For a board-material decision beyond the edge itself, see our nightstand board-material checks. Edge quality cannot compensate for a board that is unsuitable for the product’s intended use.
What to check on the physical sample
Place the sample under ordinary room light, then look along the edge rather than only at the front face. Check both ends of the strip and the points where two edged sides meet. Run a finger lightly along a permitted touch surface: a corner that catches a sleeve on a sample is unlikely to improve inside a carton.
- Coverage: is the board core fully covered on every edge specified in the drawing, including the underside or inside edge that a product photo does not show?
- Alignment: is the strip seated straight, without an obvious overhang, recessed section, or wandering joint line?
- Trimming and corners: are ends and corners clean, comfortable to touch, and consistent with the agreed profile, without chips or cuts into the panel face?
- Appearance: does the edge color, texture, sheen, and grain direction work with the face material under the lighting in which the product will be sold?
- Attachment: is there visible lifting or a gap at the end or corner? Do not treat a neat-looking surface alone as proof of long-term bond performance.
These checks should be applied to a complete assembled cabinet as well as loose panels. Assembly changes what a buyer can see and touch: an edge that looked acceptable on a bench may become the most prominent line when two faces meet.
Separate a clean appearance from bond performance
HOMAG’s edge-banding equipment descriptions show that the result depends on more than the strip itself: panel guidance, adhesive application, pressure, cutting, and trimming are all part of the process. That does not mean a buyer needs to prescribe one machine or one glue for every product. It means a perfect sample on one day is not enough evidence that later batches will be the same.
Ask the factory what it checks when it starts a run, changes an edge roll, changes a panel finish, or restarts after a stoppage. If adhesion or moisture exposure matters to the intended use, agree on a product-specific test and acceptance method with the supplier. A visual inspection can identify lifting; it cannot, by itself, establish a universal service-life or waterproof rating.
Pay attention to the cabinet’s real contact points
On a bedside cabinet, the front edge of the top is touched and seen daily. Drawer-front edges pass close to hands every time the drawer opens. A storage cabinet may have long door edges that reveal a mismatch in color or a change in trim quality more clearly than a short sample board does.
My preference is to approve these contact points on the assembled first article, not from a small loose offcut alone. Keep one signed visual reference and photograph the edges that matter from repeatable angles. The reference should include examples of an acceptable joint, corner, and color relationship, plus a short list of defects that require rework. This is the same logic behind a useful furniture golden sample: it gives production and inspection teams something concrete to compare.
Control the change from sample to shipment
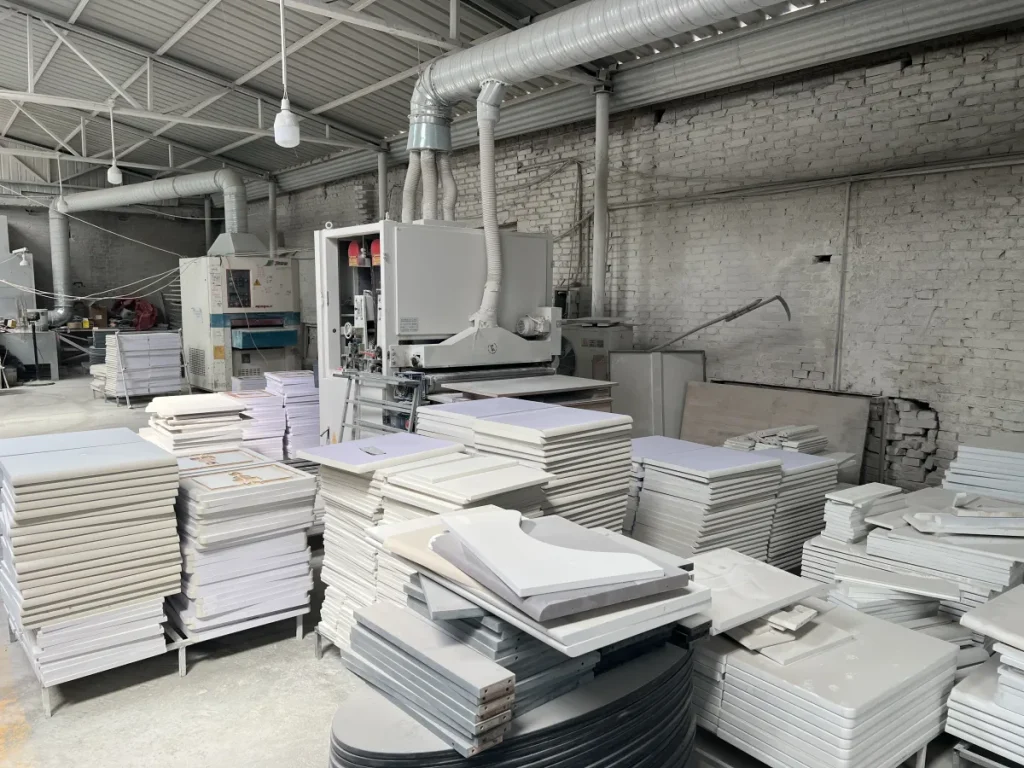
The first production panels are the point to catch a wrong strip, a changed gloss, or inconsistent trimming. Inspect a representative group before they become assembled cabinets. Then check assembled units from the run, including the back, bottom, and inner shelf edges specified in the order. If the factory uses several production lines or more than one edging supplier, agree whether each source requires its own first-article approval.
Record the edge material or reference, color, intended profile, and edge map in the order file. For repeat orders, do not assume the same product code guarantees the same result. Compare the new batch with the retained reference and approve any substitution before it reaches volume production. If a difference appears, isolate the affected panels and agree on a disposition before packing; discovering it after shipment turns a small process issue into a customer-service problem.
Edge shade is part of the wider finish conversation, especially when cabinet doors, tops, and drawers come from different runs. Our finish-color consistency checks cover that broader matching problem. Where an additional approval step affects the schedule, allow for it in the production lead-time plan instead of treating inspection as a last-minute add-on.
A short buyer sign-off
Before approving volume production, ask for five things: an edge map tied to the drawing; the agreed strip and finish reference; an assembled sample with visible and hidden edges checked; a first-run inspection point; and a written rule for substitutions and rejects. The supplier should know who can approve a change, and the buyer should know which photos or physical samples will be retained for comparison.
Good edge banding is not a promise that a cabinet can withstand any spill or environment. It is a controlled, repeatable finish on the edges people will see, touch, and judge. That is a more useful buying standard than a catalogue line that says only “edged on all sides.”